
Views: 0 Author: Site Editor Publish Time: 2026-10-13 Origin: Site


Industrial energy expenses and strict wastewater discharge limits force plant operators to rethink thermal separation and Zero Liquid Discharge (ZLD) processes. Traditional steam-driven evaporation methods, like single or multi-effect evaporators, carry unsustainable long-term operational burdens. These legacy setups demand heavy thermal energy and fail to recover latent heat efficiently. Mechanical Vapor Recompression (MVR) replaces these outdated methods, reducing energy consumption by up to 90%. We will break down the MVR Evaporator Cost from an engineering perspective. You must separate upfront capital realities from long-term operational savings and water reuse benefits. This analysis provides the technical foundation needed to evaluate system viability, select appropriate metallurgy, and accurately project return on investment without relying on volatile fossil fuel markets.
CAPEX vs. OPEX Shift: An MVR evaporator system requires a higher initial capital investment than traditional thermal systems but drastically reduces operational costs by replacing live steam with highly efficient electrical power.
Energy Efficiency Baseline: Typical electrical consumption ranges from 25 to 70 kWh per ton of evaporated water, with highly optimized systems dropping to 20–30 kWh/ton depending on feedstock characteristics.
Condensate Recovery Value: Beyond energy savings, MVR systems recover over 90% of high-quality condensate, significantly reducing raw water intake costs and municipal discharge fees.
Material and Compressor Impact: Total system cost is heavily dictated by the required materials of construction (e.g., Titanium vs. 316L Stainless Steel) and the type of mechanical compressor utilized.
Payback Period: For continuous, high-capacity industrial applications, the ROI timeline typically ranges from 1 to 3 years due to massive net annual savings in thermal energy.
Table of Contents
The initial cost of an MVR Evaporator System depends on compressor technology, heat exchanger design, construction materials, and automation requirements. Although MVR systems often require higher upfront investment than conventional steam-driven evaporators, their heat recovery capabilities can reduce long-term energy costs.
Compressor selection directly affects equipment cost and energy efficiency. Different compressor technologies suit different vapor capacities and temperature lift requirements.
Compressor Type | Main Advantage | Suitable Application |
|---|---|---|
Roots Blower | Suitable pressure rise at smaller capacities | Small to medium MVR systems |
Centrifugal Fan | High vapor flow at low pressure rise | Low-BPE evaporation |
Centrifugal Compressor | Efficient large-volume vapor compression | Large industrial MVR systems |
Heat exchanger costs depend on evaporation capacity, heat transfer area, and operating temperature differences. MVR systems often require substantial heat transfer surfaces because of their relatively small temperature driving force. Proper exchanger sizing improves efficiency while controlling equipment investment.
Material selection influences corrosion resistance, equipment lifespan, and capital costs. Aggressive wastewater containing chlorides or acids may require upgraded alloys instead of standard stainless steel.
Material | Corrosion Resistance | Relative Cost |
|---|---|---|
316L Stainless Steel | Suitable for mildly corrosive conditions | Low |
Duplex 2205 | Improved chloride resistance | Medium |
Super Duplex 2507 | High resistance to localized corrosion | High |
Titanium Grade 2 | Excellent resistance in many chloride environments | Very High |
MVR systems also require supporting components such as feed preheaters, vacuum equipment, Clean-in-Place (CIP) systems, and automated controls. PLC/SCADA systems, sensors, and Variable Frequency Drives (VFDs) help maintain stable operation and protect critical equipment.
MVR operating costs primarily include electricity, maintenance, cleaning, and auxiliary equipment operation. By recovering and reusing vapor heat, MVR technology can significantly reduce external steam demand and cooling requirements.
Electricity consumption is the main operating expense of an MVR evaporator. Depending on wastewater properties and system design, specific consumption may range from approximately 20–70 kWh per ton of evaporated water. Higher boiling point elevation and compression requirements generally increase energy demand.
MVR technology recycles secondary vapor as the heating medium, reducing the need for continuous external steam during steady-state operation. It can also reduce cooling water consumption compared with conventional multi-effect evaporation systems, helping lower utility costs.
Condensate recovery creates opportunities to reuse treated water in industrial processes, cooling systems, or equipment cleaning. Actual recovery rates and water quality depend on wastewater composition and system configuration. Additional treatment may be necessary before reuse.
Routine MVR maintenance focuses on compressor reliability, heat exchanger cleanliness, and process monitoring. Preventive inspections and scheduled cleaning help maintain energy efficiency and reduce unexpected shutdowns.
Key maintenance activities include:
Compressor Monitoring: Check vibration, bearings, and lubrication.
Heat Exchanger Cleaning: Perform CIP based on fouling conditions.
Seal Inspection: Inspect applicable mechanical sealing components.
System Monitoring: Track temperature, pressure, and energy consumption.
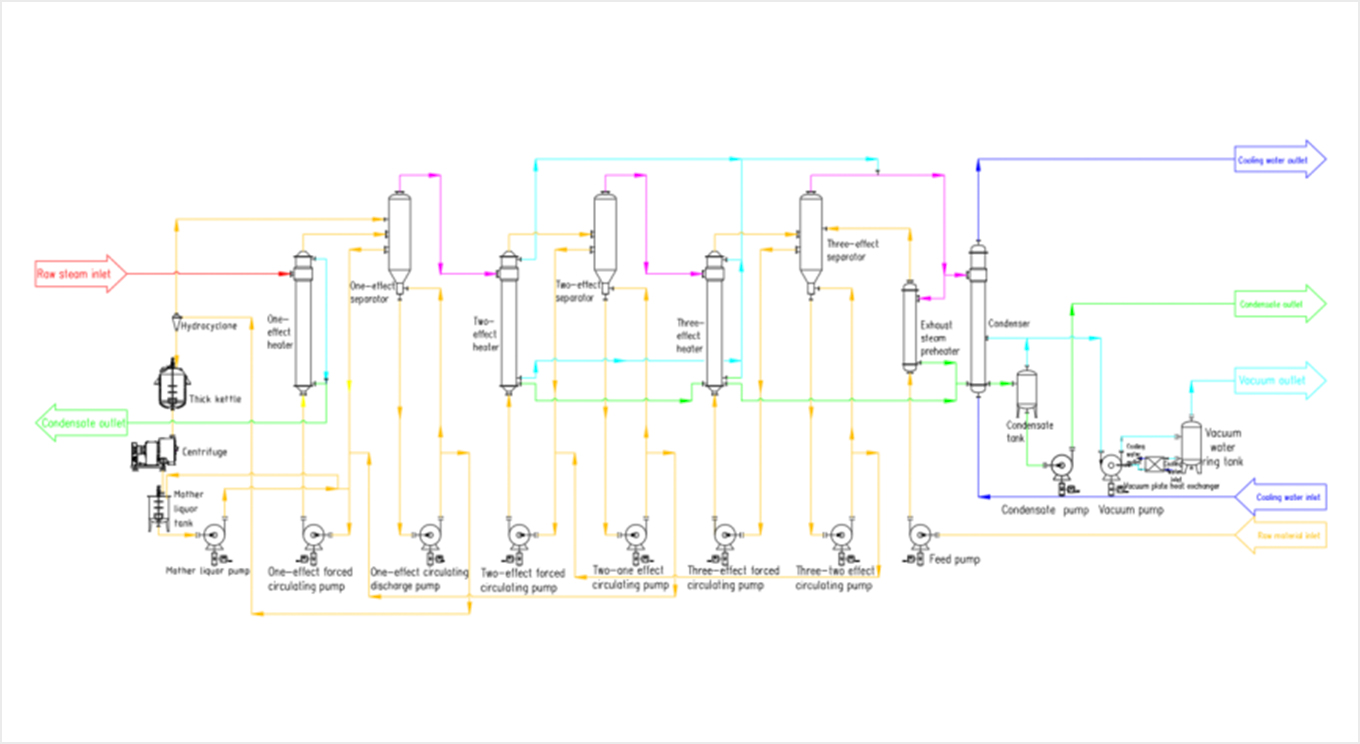
Wastewater composition directly affects MVR evaporator efficiency and equipment selection. High Boiling Point Elevation (BPE) increases compressor energy demand, while calcium, silica, and other scaling substances reduce heat transfer efficiency. Proper wastewater analysis helps optimize materials, circulation rates, and cleaning requirements.
Falling film evaporators provide efficient heat transfer for low-viscosity, low-scaling wastewater, reducing energy consumption. Forced circulation evaporators are better suited for high-viscosity, high-TDS, and crystallizing liquids, offering improved fouling resistance but requiring additional pumping energy.
MVR evaporator capacity influences equipment costs, energy efficiency, and installation requirements. Smaller modular systems simplify transportation and commissioning, while larger customized systems support higher processing volumes. Proper sizing helps balance capital investment, operating costs, and future expansion needs.
MVR systems use electrically driven compressors to recycle vapor heat, while Multi-Effect Evaporators (MEE) rely on external steam and multiple evaporation stages. MVR can reduce steam consumption and associated emissions, particularly when powered by low-carbon electricity. Economic performance depends on local utility prices and operating conditions.
MVR evaporators may require less installation space than traditional MEE systems but need sufficient electrical capacity for compressor operation. Facilities should evaluate floor space, maintenance access, transformer capacity, and electrical infrastructure upgrades before selecting equipment.

Fouling and scaling reduce heat transfer efficiency, increase energy consumption, and may cause system shutdowns. Proper circulation velocity, suitable heat exchanger design, and automated Clean-in-Place (CIP) systems help control deposits and maintain stable MVR performance.
Compressor reliability is essential for continuous MVR operation. Mechanical wear, vibration, or bearing failures can interrupt wastewater treatment. Preventive maintenance, vibration monitoring, critical spare parts, and optional standby equipment help reduce unexpected downtime.
MVR systems require trained operators to manage compressor performance, wastewater concentration, and automated controls. Training in SCADA monitoring, startup procedures, load adjustments, and emergency shutdowns helps maintain operational stability and minimize equipment damage.
MVR return on investment (ROI) depends on equipment costs, steam prices, electricity rates, evaporation capacity, and annual operating hours. Additional savings may come from recovered water, reduced wastewater disposal, and lower cooling system requirements. Accurate cost data supports reliable financial evaluations.
For an MVR evaporator processing 10 tons of water per hour at 35 kWh/ton, estimated electrical demand is 350 kW. Operating 8,000 hours annually results in approximately 2.8 million kWh of electricity consumption. Actual savings and payback depend on local energy prices, capital investment, maintenance costs, and performance compared with existing evaporation equipment.
Transitioning to mechanical vapor recompression requires careful engineering analysis and financial planning. To move forward with an installation, execute the following steps:
Audit your current thermal energy consumption and map it against local electrical utility rates to determine baseline economic feasibility.
Analyze your specific wastewater or product chemistry to identify the required metallurgy and potential boiling point elevation constraints.
Engage with specialized engineering firms to conduct pilot testing, ensuring the selected compressor and heat exchanger configuration matches your exact fluid dynamics.
Build a comprehensive financial model that accounts for total operational savings, including eliminated steam, recovered water, and avoided disposal fees, to secure project funding.
A: The industry average ranges from 25 to 70 kWh per ton of evaporated water. Highly optimized falling film systems treating low-viscosity, low-boiling-point-elevation fluids can achieve efficiencies between 20 and 30 kWh per ton.
A: The higher initial cost stems from the expensive mechanical compressor, the need for significantly larger heat exchanger surface areas due to low temperature differences, and the sophisticated automation required to manage turbomachinery.
A: Yes, but it requires upgrading the materials of construction. Handling high chlorides or aggressive acids necessitates using Duplex stainless steel, Super Duplex, or Titanium, which significantly increases the equipment cost.
A: Compressors require strict routine maintenance, including regular oil changes, mechanical seal inspections, bearing replacements, and continuous vibration monitoring to prevent catastrophic failures and ensure long-term reliability.
A: High BPE means the fluid boils at a higher temperature than pure water. This forces the compressor to achieve a higher compression ratio to maintain heat transfer, requiring more robust equipment and increasing electrical power consumption.
A: For continuous operations running 24/7, the massive reduction in thermal energy costs usually results in a payback period of 1 to 3 years, depending on local electricity rates and the eliminated costs of live steam.

